How to Calculate Molding Pressure for Plastic Injection
Molding pressure determines how completely molten plastic fills a cavity before the gate freezes. It also affects flash, sink marks, weld lines, part weight, and dimensional stability. This matters across a large industry. PlasticsEurope’s Plastics—The Fast Facts 2023 reported global plastics production of 400.3 million tonnes in 2022. Even small pressure errors can therefore create significant material waste and inconsistent production.
John P. Beaumont, a recognized injection-molding author and process specialist, describes injection molding as “a pressure-driven process.” His statement provides a useful starting point. Molding pressure is not simply the hydraulic pressure displayed on a machine. Engineers must consider cavity pressure, projected area, melt viscosity, flow length, gate design, temperature, and pressure losses through the runner system. A practical calculation often begins with required cavity pressure multiplied by projected part area. The result then needs comparison with the machine’s available injection pressure and clamp force.
A neat formula can still mislead. Resin data may come from controlled laboratory tests, while a real mold contains corners, weld lines, and cooling differences. ASTM D3835 and material supplier datasheets can support a more reliable assessment. Process records should confirm the calculation using cavity-pressure sensors, part weight, and short-shot trials. This guide explains each step clearly, from unit conversion to safety factors. It also highlights where assumptions deserve review, because an apparently safe molding pressure may fail when material temperature, moisture, or cycle speed changes.
Define Injection Pressure, Cavity Pressure, and Clamp Force in MPa
How to Calculate Molding Pressure for Plastic Injection
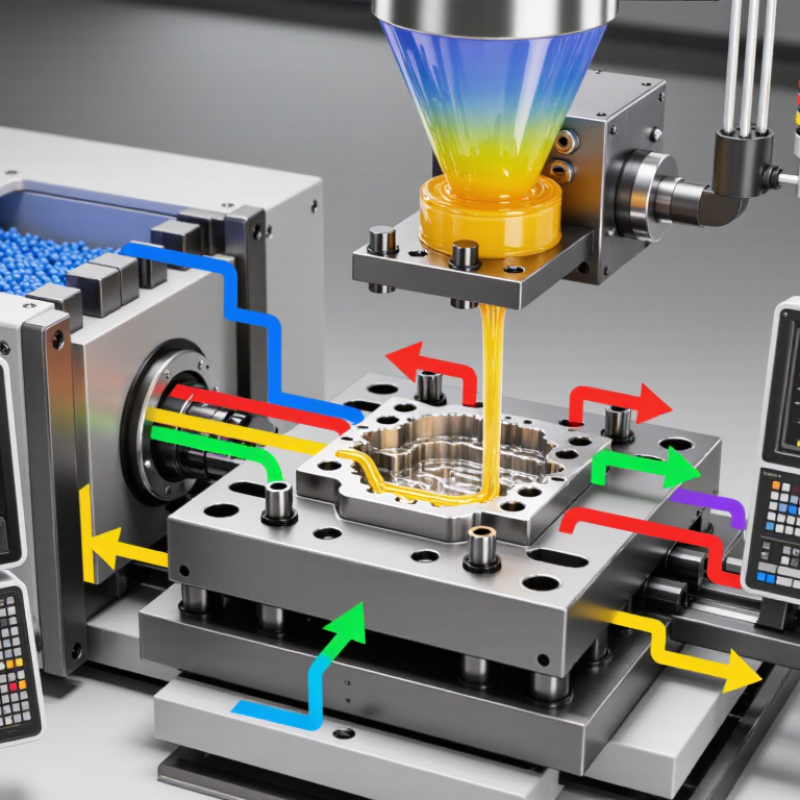
Injection pressure is the hydraulic or screw pressure needed to push molten plastic through the nozzle, runner, and gate. It is usually higher than the pressure inside the mold cavity because flow resistance consumes pressure. In practical molding, pressure is measured in MPa. A machine setting of 120 MPa does not mean the cavity receives 120 MPa. Cavity pressure is the pressure acting directly on the mold surface and part geometry. Sensors near the gate provide more reliable data than machine settings alone.
Clamp force prevents the mold from opening during filling. A practical estimate uses this formula: clamp force (kN) = cavity pressure (MPa) × projected area (mm²) ÷ 1,000. Add a suitable safety margin for pressure peaks, uneven filling, and material variation. For example, 45 MPa acting on 8,000 mm² requires about 360 kN before the safety factor. This is only an estimate. Thin walls, long flow paths, and restricted gates can raise actual pressure significantly.
Tips: Record cavity pressure during stable production, not only during machine setup. Check flash, short shots, and part dimensions together. If the result looks strange, question the sensor position and projected-area calculation. A calculator can be correct while the assumptions remain wrong. Use trial data, mold analysis, and qualified process review before selecting final clamp force.
Select a Baseline: PP 50–100, ABS 70–120, and PC 100–150 MPa
How to Calculate Molding Pressure for Plastic Injection
Select a baseline before changing machine settings. Industry processing surveys and technical data sheets from 2023–2024 commonly place PP at 50–100 MPa, ABS at 70–120 MPa, and PC at 100–150 MPa. These values describe injection pressure, not automatically cavity pressure. In practical terms, the PP range equals roughly 500–1,000 bar at the machine hydraulic system.
Start near the middle of the suitable range. For PP, 75 MPa is a reasonable trial point. ABS may begin near 95 MPa, while PC often requires about 125 MPa. Then inspect short shots, weld lines, flash, and part weight. A mold filling report following ISO 294-1 principles can help confirm whether the selected pressure supports stable filling. Wall thickness, flow length, melt temperature, gate size, and recycled content can shift the requirement significantly.
Do not chase the highest number.
Higher pressure may hide poor venting or an undersized gate. It can also increase flash, stress, and mold deflection. My shop-floor experience suggests adjusting in small steps, usually 5–10 MPa, while recording fill time and peak pressure. The baseline is useful, but it is not sacred. Pressure readings can differ between machines, and that inconsistency deserves a second measurement before production approval.
How to Calculate Molding Pressure for Plastic Injection - Select a Baseline: PP 50–100, ABS 70–120, and PC 100–150 MPa
| Material |
Baseline Injection Pressure |
Equivalent Pressure |
Typical Material Characteristics |
Starting-Point Guidance |
Important Adjustment Factors |
| Polypropylene (PP) |
50–100 MPa |
500–1,000 bar
7,250–14,500 psi |
Generally good flow, relatively low viscosity, and moderate shrinkage. |
Begin near the middle of the range, then increase pressure only as needed to fill the cavity and pack critical areas. |
Part wall thickness, flow length, gate size, melt temperature, mold temperature, glass-fiber content, and venting quality. |
| Acrylonitrile Butadiene Styrene (ABS) |
70–120 MPa |
700–1,200 bar
10,150–17,400 psi |
Moderate flow resistance with good dimensional stability and surface quality when processed correctly. |
Use a moderate initial setting and raise pressure gradually if short shots, sink marks, or insufficient packing occur. |
Grade viscosity, melt and mold temperature, flow-path length, wall thickness, gate restriction, and moisture control. |
| Polycarbonate (PC) |
100–150 MPa |
1,000–1,500 bar
14,500–21,750 psi |
High melt viscosity and comparatively high resistance to flow; careful drying and temperature control are important. |
Start toward the lower or middle portion of the range when the mold has adequate gates and short flow paths; increase as required for complete filling. |
High melt viscosity, long flow length, thin walls, mold temperature, melt temperature, gate design, and resin moisture. |
Practical calculation:
Required Clamp Force (N) = Projected Area (mm²) × Cavity Pressure (MPa) × Safety Factor.
Include the projected area of the part and runner system. A commonly used preliminary safety factor is approximately 1.1–1.2, but the final value should be verified through molding trials and machine capability checks. Injection pressure is a starting range, not a universal setting; the actual requirement depends on the resin grade, mold design, part geometry, and process conditions.
Calculate Clamping Force with F = P × A and 2–5 tons/in²
Clamping force prevents the mold from opening during plastic injection. Use F = P × A to estimate the required force. F is clamping force in tons, P is estimated pressure in tons per square inch, and A is projected area in square inches. For many molding jobs, engineers begin with 2–5 tons/in² as a practical working range.
Measure the part’s projected area on the parting line, including runners, gates, and other projected features. Do not use the total surface area. A mold with a 20 in² projected area may need 60 tons at 3 tons/in². The same mold could require 100 tons at 5 tons/in². Keep it simple.
Pressure selection needs judgment. Thin walls, long flow paths, glass-filled materials, and difficult gates may push the estimate toward 5 tons/in². Thick sections and shorter flow paths may need less. Injection pressure is not the same as clamping pressure. That mistake is common. A safety margin of about 10–15% can help cover process variation, but excessive force may stress the mold or machine. During trials, inspect the parting line for flash and check cavity filling. Flash can indicate insufficient force, poor venting, mold wear, or uneven alignment. A rough estimate can look convincing and still be wrong. Confirm the calculation against machine specifications, tie-bar limits, and actual molding results.
Verify Pressure Using Fill Time, Pressure Curves, and Molded-Part Quality
How to Calculate Molding Pressure for Plastic Injection
Estimate molding pressure by studying material flow, cavity geometry, and projected part area. A useful starting point is injection pressure multiplied by projected area. This value helps estimate clamp force, but it does not replace a cavity-pressure measurement. Thin walls, long flow paths, cold molds, and restrictive gates can raise pressure sharply.
Fill time provides an early warning. Record the time from screw movement to cavity filling, then compare it with the process target. A longer fill time may indicate excessive resistance, low melt temperature, or insufficient injection speed. A very short fill time can create jetting, trapped air, or unstable pressure. Small changes matter.
Use the pressure curve as evidence. A smooth rise usually shows consistent filling. Sudden peaks may reveal a blocked gate, poor venting, or an aggressive speed change. Place pressure sensors near critical flow ends when possible. My first calculation is often optimistic. Real molds rarely behave like simple equations.
Check the molded part after each adjustment. Look for short shots, flash, sink marks, weld lines, and uneven gloss. Measure dimensions after cooling, not immediately after ejection. If cavity pressure is stable but parts still vary, investigate material moisture, mold temperature, or cooling balance. Data can expose mistakes. It cannot replace careful observation.