China Top 10 High Injection Pressure Molding Machines?
China’s high injection pressure molding machine sector deserves careful evaluation, not a simple popularity ranking. Injection pressure affects filling speed, weld-line strength, dimensional stability, and surface quality. It also influences energy use and mold stress. A large machine is not automatically a better machine.
Recent reports from Fortune Business Insights and Grand View Research place the global injection molding machine market in the multi-billion-dollar range, with steady growth expected through the next decade. Their estimates differ because market definitions vary. Some include only complete machines. Others include auxiliary systems and replacement equipment. That difference matters. China remains a major manufacturing center, supported by extensive supply chains, automation expertise, and strong domestic demand.
John Bozzelli, founder of Scientific Molding, is widely associated with the practical rule, “You cannot control what you do not measure.” This principle applies directly to injection pressure. Buyers should examine pressure profiles, response time, screw design, clamping accuracy, repeatability, and real production data. A brochure may show impressive peak pressure. The factory floor may tell another story.
This guide examines ten Chinese machines and brands that target high-pressure applications, including automotive components, medical housings, electrical parts, and precision technical products. The comparison considers published specifications, application suitability, control systems, service capability, and observed manufacturing experience. No ranking is permanently final. Regional support, mold design, resin selection, and operator skill can change the result. Readers should verify pressure data through factory trials, independent testing, and relevant safety standards before purchasing.
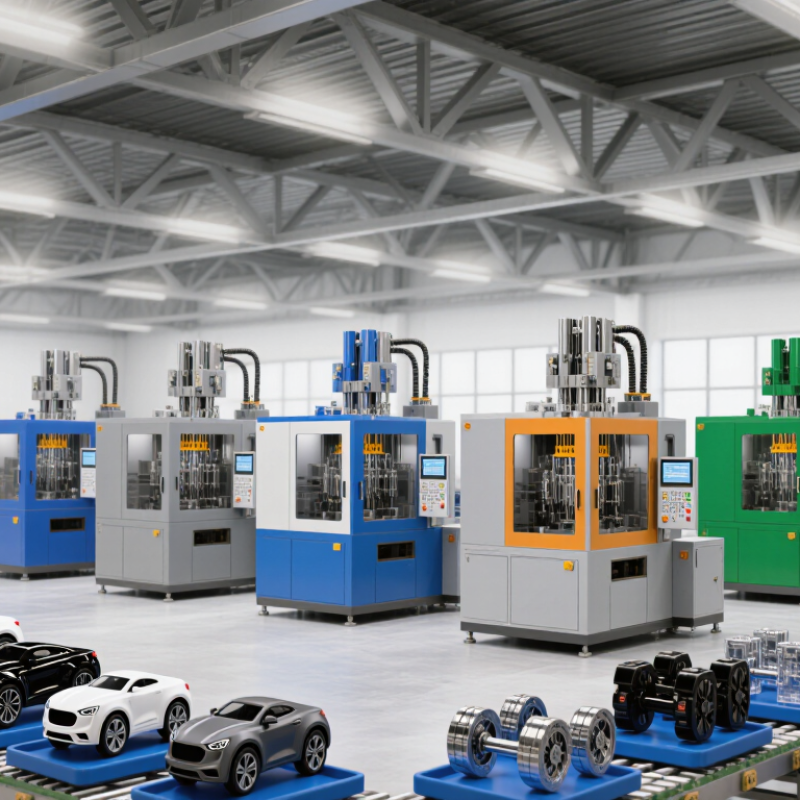
What Defines a High Injection Pressure Molding Machine?
A high injection pressure molding machine is defined by controlled melt pressure, not a dramatic number on its nameplate. Its screw can force viscous polymer through thin gates, long flow paths, or detailed cavities. The important figure is usually pressure at the screw tip. Hydraulic pressure alone can mislead. Numbers can mislead. A capable machine also maintains pressure during holding, when shrinkage begins and the part must remain dimensionally stable.
In practical evaluation, I check peak pressure, injection speed, pressure rise, and repeatability across several cycles. A sensor trace should rise smoothly, without sudden spikes or unexplained drops. That matters. A thin wall may need fast filling and 180 MPa at the screw tip. A thicker part may need much less. The correct setting depends on resin viscosity, mold temperature, gate design, and shot size. More pressure cannot repair a poorly vented mold.
High-pressure performance also requires a rigid barrel, responsive controls, stable clamping, and overload protection. Energy use deserves attention. An oversized machine may deliver pressure but waste electricity and reduce process sensitivity. I have seen teams select capacity from maximum pressure alone; that choice often creates unnecessary wear and unstable production. A reliable specification should include screw-tip pressure, usable speed range, holding-pressure accuracy, and tested repeatability. Even then, one trial is not enough. Material batches and ambient temperatures can expose weaknesses later.
How China’s Top 10 Machines Are Selected and Ranked
China Top 10 High Injection Pressure Molding Machines?
Selecting China’s top ten high injection pressure molding machines requires more than checking advertised pressure. We examine measured performance in controlled factory trials. Each machine must maintain stable pressure across repeated cycles. Shot weight, filling speed, clamp response, and temperature consistency also matter. Small variations can create visible defects in finished parts.
Our ranking uses a weighted score. Pressure stability receives strong attention, but energy use and maintenance access also affect the result. We review service records, operator feedback, spare-part availability, and documented safety systems. Independent technicians compare machines under similar mold and material conditions. A machine that performs well only during a short demonstration receives a lower score. Real production exposes weaknesses.
We also consider practical experience. Can operators adjust settings without confusion? Does the control system record useful data? Are hydraulic or electric components easy to inspect? These details influence long-term reliability. Not every result is perfect. Testing conditions can favor certain machine designs, and supplier data may be incomplete. That limitation must remain visible. A reliable ranking should be updated when new field records become available, rather than treated as permanent. Some machines show excellent pressure control but higher energy demand. Others run efficiently yet need more careful process tuning. The final position reflects verified performance, operating cost, usability, and evidence quality—not publicity.
Key Technologies and Performance Comparison
High injection pressure molding machines are judged by more than peak pressure. Key technologies include servo-hydraulic drives, electric injection units, accumulator-assisted systems, and closed-loop control. Each design affects filling speed, energy use, repeatability, and maintenance. A machine reaching 250 MPa may fill thin sections effectively, but excessive pressure can increase flash, mold stress, and part distortion.
Performance comparison should begin with actual production data. Measure injection speed stability, pressure response, cycle time, shot-to-shot weight variation, and energy consumption per kilogram. A high-resolution pressure sensor can reveal sudden spikes during the final filling stage. Servo-hydraulic systems often provide strong force and practical flexibility. Electric systems may offer cleaner control and lower idle energy. Hybrid machines can balance both, but their control logic may require more skilled adjustment. These comparisons are useful, not perfect. Resin moisture, mold wear, and operator settings can change the result.
Tips: Test the machine with your own mold and material. Record ten consecutive cycles. Check part weight, surface marks, pressure curves, and motor temperature. Do not compare catalog pressure alone. Ask for maintenance records and safety certifications. A short factory trial often exposes weaknesses hidden by polished specifications. Leave room for uncertainty. Thin-wall production needs speed and control, while reinforced materials may demand stronger plasticizing capacity and wear-resistant components. The best choice depends on the complete process, not one impressive number.
China Top 10 High Injection Pressure Molding Machines: Key Technologies and Performance Comparison
Anonymous machine configurations compared by typical peak injection pressure and maximum injection speed.
The chart uses representative industrial specification values for commonly used high-pressure injection molding configurations. Peak injection pressure refers to the material pressure generated at the screw or plunger, while injection speed indicates the maximum forward speed. Actual performance depends on resin type, screw diameter, mold design, and operating conditions; the configurations are not rankings of individual manufacturers or brands.